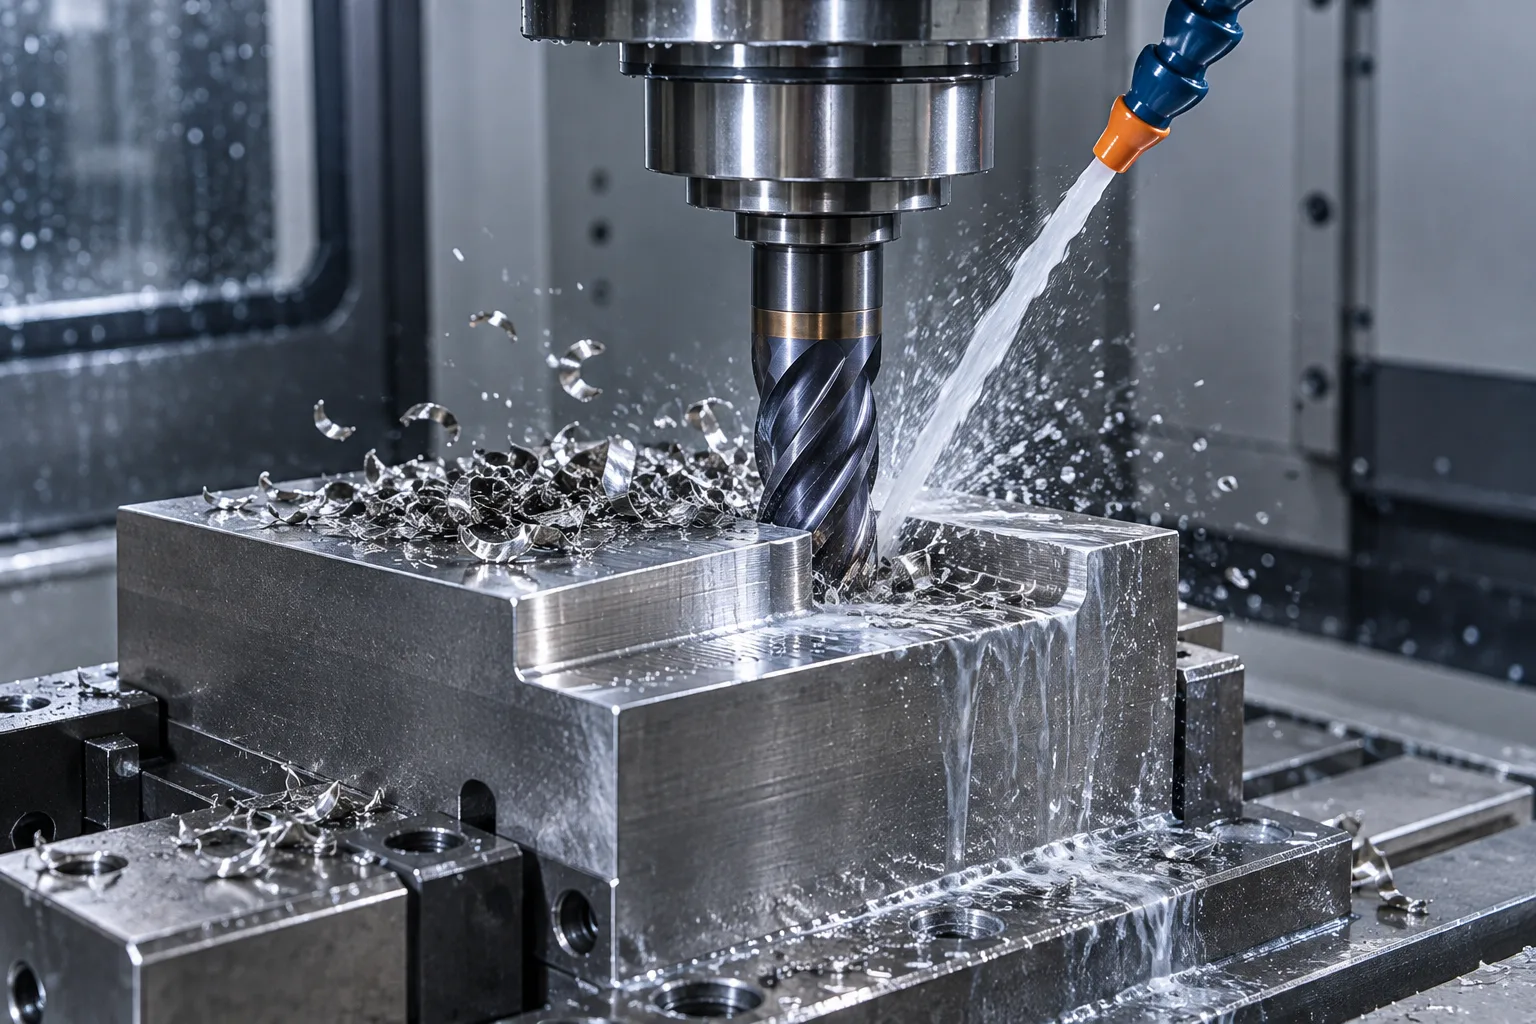
To improve tool life in CNC milling, diagnose wear before changing cutting data: match the cutter to the workpiece, keep a verified chip load, control heat and chips, and check runout and support. This guide gives a repeatable check sequence for production and first trials.
Start with the wear symptom
| Observed symptom | Checks to make first | Likely direction |
|---|---|---|
| Flank wear grows steadily | Speed, chip load, coolant and abrasive workpiece constituents | Confirm grade/coating and reduce thermal load only after checking the data |
| Chipping or broken edge | Interrupted cut, runout, workholding, radial engagement and edge preparation | Improve support and reduce shock before selecting a tougher edge |
| Built-up edge or rubbing | Feed per tooth, sharpness, material and chip evacuation | Restore a real chip load and clear recut chips |
| Poor finish with little visible wear | Runout, tool projection, deflection, machine condition and programming | Stabilize the assembly before blaming the insert or coating |
These symptoms are diagnostic clues, not proof of one cause. Record the workpiece grade, cutter geometry, flute count, coating, projection, coolant method and part count with every trial.
Match cutter geometry to the workpiece
Aluminum and other non-ferrous alloys often need a sharp cutting edge and adequate flute space for chip evacuation. Carbon steel and stainless steel usually require a grade and coating selected for their heat, adhesion and wear behaviour. Hardened materials may need stronger edge preparation and lower engagement. Use the manufacturer’s data for the exact cutter and material; do not copy a speed or tool-life claim from a different diameter, flute count or coating.
When comparing a milling tool family or an individual square milling insert, confirm the insert or cutter geometry, available grades and the intended operation. A product category can contain roughing, finishing and high-feed geometries that should not share one starting recipe.
Set chip load before chasing tool life
Start from the tool maker’s recommended surface speed and feed per tooth. Calculate feed rate from the number of flutes and the selected chip load, then adjust for radial engagement, axial depth, machine power and rigidity. Feed that is too low can rub instead of cut; excessive feed can overload the edge. If the radial engagement changes substantially, recheck the recommended chip load rather than applying the same feed blindly.
Runout matters because one flute can carry more load than the others. Clean the holder and tool shank, measure runout at the cutting edge where practical, and verify the gauge length. A short, rigid setup generally gives the cutting edge a more repeatable load path than an unnecessarily long projection.
Control heat and chip evacuation
Keep chips away from the cutting edge. Use through-tool coolant, a directed external stream or air when the tool and workpiece permit it. Deep pockets and long slots can trap chips; consider a toolpath that maintains a stable engagement and reduce radial engagement when the machine and tool maker’s recommendations call for it. Coolant flow is not a substitute for suitable geometry or a verified cutting condition.
Use a controlled wear trial
- Measure the new tool and record the tool number, projection and runout.
- Run a defined part count with one material and one documented cutting condition.
- Inspect flank wear, edge chipping, burrs, finish and spindle load at fixed intervals.
- Change one variable at a time: speed, feed, engagement, coolant or geometry.
- Stop when the agreed quality limit is reached and record the usable part count.
This method separates tool wear from workholding movement, machine vibration and chip packing. It also creates application evidence for a supplier recommendation instead of relying on a universal tool-life number.
Technical basis and limitations
BIG DAISHOWA’s machining vibration guidance supports checking tooling-assembly length, rigidity and engagement, and maintaining consistent chip thickness. The symptom table above is a general diagnostic workflow, not a test report or a one-cause diagnosis. No cutting values or tool-life improvement percentages are claimed; confirm grade-specific cutting data with the cutter manufacturer.
Frequently asked questions
Does a harder coating always increase milling tool life?
No. Tool life depends on the workpiece, cutting temperature, edge preparation, chip load, engagement and coolant. Confirm the coating and grade for the actual application.
Should I lower feed when a tool starts to wear?
First identify whether the wear is thermal, abrasive, adhesive or impact-related. Lowering feed can increase rubbing; use the tool maker’s recommendations and change one controlled variable.
What information should I send for a tool-life recommendation?
Send the workpiece grade and hardness, operation, cutter or insert geometry, diameter, flute count, projection, speed, feed, engagement, coolant method, part count and observed wear.
For related selection help, review how to choose a milling cutter and the Wujinniu CNC tooling team information. Technical guidance is application-specific and does not promise a fixed tool life.