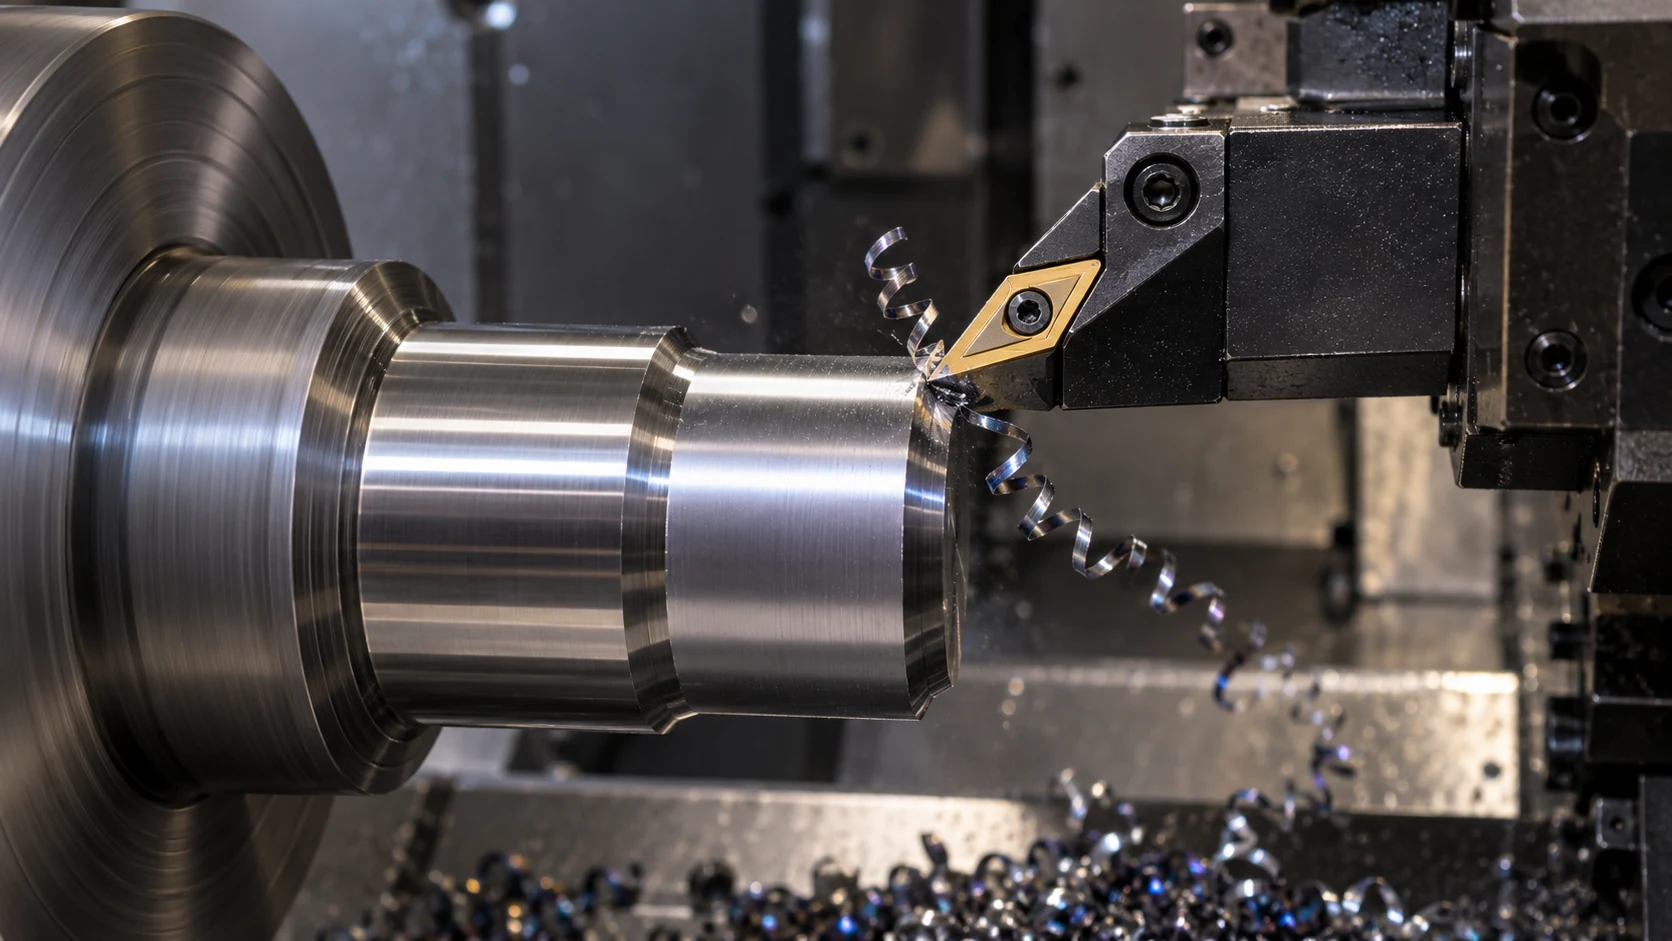
An MVVNR/L 72.5° tool holder with a VNMG1604 insert is used for robust CNC lathe turning. Setup quality depends on tool orientation, insert seating, workholding rigidity and cutting data matched to the workpiece.

Check orientation and center height
Install the holder in the correct right- or left-hand orientation and set the cutting edge on center. Incorrect height changes the effective geometry and can increase cutting force or reduce surface quality.
Seat the VNMG1604 insert correctly
Clean the pocket, screw and insert before assembly. The insert must sit fully against the locating surfaces with the correct screw torque. Do not run a damaged or chipped insert in a heavy cut.
Choose roughing and finishing data
Use a stable roughing pass for steel, cast iron or alloy parts, then reduce depth of cut and feed for finishing. Confirm speed, feed, nose radius and coolant through a controlled trial.
Reduce vibration in production
Keep tool overhang short, secure the workpiece and check turret alignment. If chatter persists, reduce radial engagement or adjust speed before increasing feed.
Frequently Asked Questions
Which insert does this holder use?
The product is specified for VNMG1604 inserts; confirm the exact grade and chipbreaker for the workpiece.
What machines are compatible?
It is intended for CNC lathes with the matching tool station and holder orientation.
For product specifications, see MVVNR/L 72.5° Heavy-Duty Lathe Tool with VNMG1604 Inserts for CNC Turning.
Technical information is prepared by the Wujinniu CNC tooling team based on product application data and machining requirements.