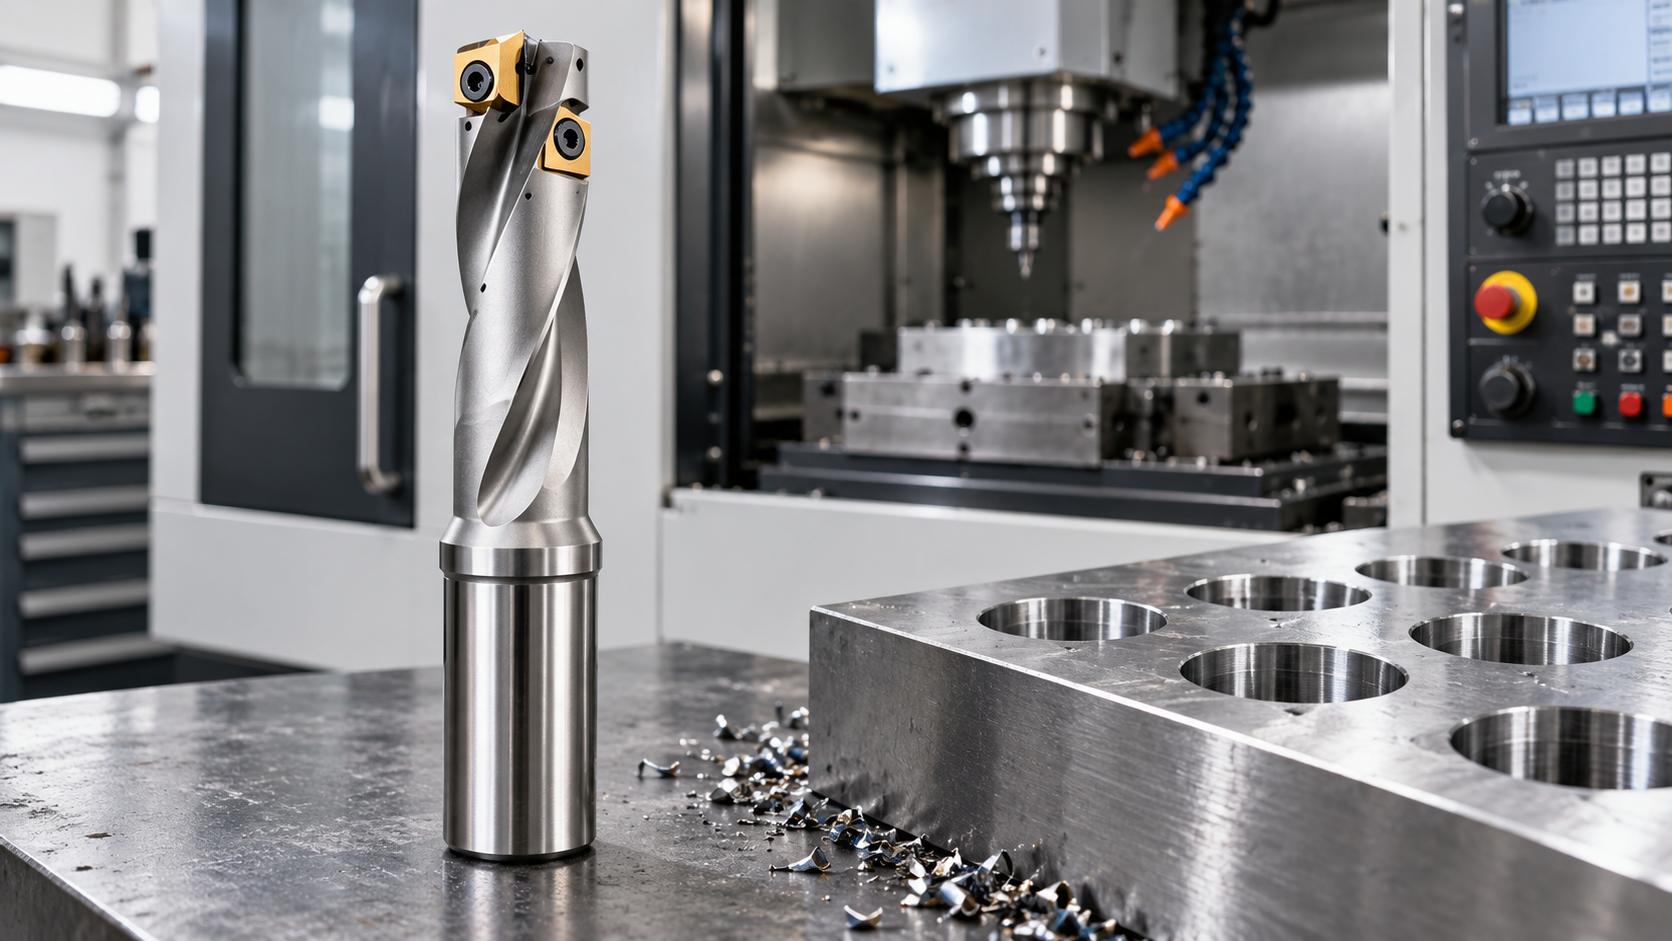
A WD-U indexable drill is selected as a complete CNC holemaking system, not only by the word “drill.” The body, straight shank, insert seat, diameter range, workpiece and machine interface must work together. This guide explains the confirmed WD-U information and the checks needed before production drilling.

What is a WD-U indexable drill?
A WD-U indexable drill uses replaceable carbide inserts in a dedicated drill body. The replaceable insert format can simplify routine maintenance, but the insert geometry and locating surfaces must match the body. A similar-looking insert or holder should never be assumed compatible without a drawing or manufacturer confirmation.
Confirmed WD-U specifications
The local Wujinniu WD-U Indexable Drill System listing identifies the model as WD, an H13 body material, a 12–100 mm diameter range, a straight shank and CNC machining in steel and cast iron. The record also lists a plastic box package and a three-year warranty. These facts apply to that listing; confirm the exact size and configuration before ordering.
How to choose the diameter
Start with the finished hole diameter and tolerance. Select a WD-U size that covers the required hole without relying on an unconfirmed allowance. Hole depth, entry condition, interrupted surfaces and machine rigidity can change the practical choice. If the required diameter is outside the listed 12–100 mm range, request an alternative configuration rather than assuming the WD-U system covers it.
Straight-shank and machine compatibility
A straight shank must match the holder, collet or chuck used on the CNC machine. Confirm shank diameter, usable clamping length, runout and the available coolant path. Secure clamping is especially important when the tool is extended or when the hole is deep. The straight-shank description alone does not define a complete machine interface.
Insert, coolant and chip control
Match the insert grade and chipbreaker to the workpiece and application. Steel and cast iron may require different edge preparation or cutting data. Confirm coolant direction and chip evacuation before production. Use the manufacturer’s speed and feed chart; do not infer cutting data from the WD model or nominal diameter alone.
WD-U setup checklist
- Confirm finished diameter, tolerance and hole depth.
- Confirm the straight-shank holder and clamping length.
- Check insert geometry, grade, seat and screw or clamp.
- Confirm machine rigidity, runout and coolant delivery.
- Run a first-hole inspection for size, roundness, finish and chips.
Frequently Asked Questions
What diameter range is confirmed for the WD-U listing?
The local listing confirms 12–100 mm. Confirm the exact available diameter and drawing for the order.
Can the WD-U drill machine stainless steel?
The confirmed listing names steel and cast iron. For stainless steel, confirm a suitable insert grade and application recommendation with the manufacturer.
Does a straight shank fit every CNC holder?
No. Match the shank and clamping dimensions to the actual holder or collet.
Related resources: U Drills | WD-U product
Technical information is prepared by the Wujinniu CNC tooling team based on product application data and machining requirements.